
Stainless Steel Specialists
Pipe Fittings
Stainless steel and corrosion-resistant alloys. Butt-weld, threaded, and socket-weld fittings in NPS 1/4" through 36" across ASME B16.9, B16.11, and B16.28.
Standards: ASME B16.9 · B16.11 · B16.28
Sizes: 1/4" – 36" NPS
Classes: 150 · 3000 · 6000
Overview
What We Stock
Pipe fittings change direction, branch a line, reduce or expand pipe size, and cap or close runs. Unified Alloys stocks fittings in the same alloys, grades, and dimensional schedules as our pipe — austenitic stainless across the standard B16.9 butt-weld range, forged Class 3000 and 6000 in B16.11 for threaded and socket-weld service, and MSS-spec outlets and swages for branch connections.
The fitting type sets the standard. Butt-weld fittings cover the full size range from 1/2″ through 36″ NPS and are produced to ASME B16.9 and B16.28. Threaded and socket-weld fittings are limited to 2″ NPS and below, produced to ASME B16.11 in Class 3000 and 6000 forgings. Outlet fittings (weld, threaded, socket, lateral, elbow, nipple) follow MSS SP-97. Each connection type is appropriate for different service conditions, pressures, and pipe sizes — we cover the trade-offs further down this page.
For mechanical and coupling-based fittings (Victaulic, Teekay, and similar grooved or pressed systems), see Mechanical Piping Systems.
Class 6000 forged fittings, chrome moly grades, and non-standard configurations are quoted on request. Sizes above 36" NPS in butt-weld and reducers of greater reduction than covered by ASME B16.9 are available on order.
Key Applications
- Elbows — 90°, 45°, and 180° returns in long radius or short radius
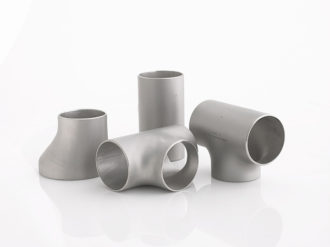
- Tees — straight and reducing branches
- Reducers — concentric and eccentric
- Caps and stub ends
- Outlets — weld, threaded, socket, lateral, elbow, and nipple configurations
- Swages — forged in concentric and eccentric shapes
- Nipples, couplings, plugs, bushings, and unions in screwed or socket-weld
Materials & Grades
Available Materials
Fittings are stocked across austenitic stainless and supplied on request in higher-alloy and chrome moly grades. All material conforms to ASTM A403 / ASME SA403 for butt-weld fittings, ASTM A182 / ASME SA182 for forged fittings, and can be supplied with MTRs traceable to the heat number.
Core stocking range. Standard for corrosion resistance in chemical processing, refining, food-grade, and general industrial pressure service.
304 · 304L · 316 · 316L · 317L · 321 · 347
For chloride-rich service, seawater, and high-strength applications where standard austenitics fall short.
2205 · 254SMo
For severe corrosion environments, high temperatures, and aggressive chemical service.
Monel · Inconel
For high-temperature power and process service (steam, refinery heater lines) under ASME B31.1 / B31.3 code.
P5 · P9 · P11 · P22 · P91
Connection Type
Butt-Weld, Threaded & Socket-Weld
Three connection types cover effectively all pipe fitting service: butt-weld for the full size range, threaded and socket-weld for small-bore applications. Each is produced to a different standard and serves different conditions.
Butt-Weld
Butt-weld fittings (ASME B16.9 / B16.28) are the workhorse for piping 2″ NPS and above, and are supplied across the full range from 1/2″ through 36″. The ends are bevelled to match the pipe weld preparation, producing a continuous flow path with no internal disruption. This is the standard for pressure piping, process service, and any application where flow characteristics and full pipe-equivalent strength matter.
Threaded
Threaded fittings (ASME B16.11) are used for small-diameter pipe sizes 2″ NPS and below. The majority carry female NPT threads per ASME B1.20.1. Cast Class 150 is suitable for air and water at low temperature and pressure. Forged Class 3000 and 6000 are used for higher pressures, higher temperatures, and more complex media. Threaded fittings remove the need for site welding but introduce a leak path that butt-weld doesn’t have, which limits them in critical service.
Socket-Weld
Socket-weld fittings (ASME B16.11) are also limited to 2″ NPS and below, and bridge the gap between threaded and butt-weld. The pipe slips into a deep socket on the fitting; the weld is made on the outer surface. This avoids a leak path while still working at small pipe sizes where butt-welding becomes impractical. Class 3000 and 6000 are the typical stainless stocking range.
The connection type drives both standard and size availability. Threaded and socket-weld are limited to 2" NPS and below in stainless. Above 2", the question becomes butt-weld in B16.9 and B16.28, full stop. Confirm requirements with your piping engineer before ordering.
Technical Data
Dimensional References
Pipe fittings cover multiple ASME and MSS dimensional standards. Each connection type and fitting category has its own reference page below — dimensions, weights, tolerances, and downloadable PDFs.
Butt Weld Fittings : ASTM A403 / ASME SA403 – B16.9 – B16.28
Full dimensional data by pressure class
Forged Lateral Connection : ASTM A182 / ASME B16.9 – B16.11 – B16.25
Full dimensional data by pressure class
Class 3000 / 6000 Forged Outlet Fittings : ASTM A182 / ASME B16.11 / MSS SP-97
Full dimensional data by pressure class
Forged Swage Nipples : ASTM A403 / MSS SP-95
Full dimensional data by pressure class
Class 3000 / 6000 Forged Fittings : ASTM A182 / ASME SA182 – B1.20.1
Full dimensional data by pressure class
Basic Dimension of National Standard (NPT) Pipe Threads : ASME B1.20.1
Full dimensional data by pressure class
Stainless Steel Pipe Nipples : ASTM A312 / ASME SA312 – ASME B1.20.1
Full dimensional data by pressure class
Regulatory & Traceability
CRN & Material Traceability
Pipe fittings are pressure-containing components and are commonly registered as fittings in their own right under Canadian Registration Number (CRN) programs in Alberta, British Columbia, Saskatchewan, Ontario, and other provinces. CRN-stamped fittings come with a registration mark traceable to the registered design, and supply documentation must support both the registration and the underlying material specification.
Mill Test Reports (MTRs) traceable to the heat number can be supplied with orders, confirming chemical composition, mechanical properties, and conformance to ASTM A403 / SA403 for butt-weld and ASTM A182 / SA182 for forged fittings. NACE conformance (MR0175 / MR0103 for sour service) and Positive Material Identification (PMI) are available on request — confirm requirements at the time of quote.
If you’re unsure whether a specific fitting type, size, or class requires CRN registration for your application or jurisdiction, our technical sales team can advise.
FAQ
Frequently Asked Questions
When do I use butt-weld vs threaded vs socket-weld?
Size sets most of the answer. Above 2″ NPS, butt-weld is effectively the only choice — threaded and socket-weld stainless fittings aren’t stocked above 2″. Below 2″ the call comes down to service conditions. Threaded is fastest to assemble in the field but introduces a leak path, which limits it in pressure or critical service. Socket-weld eliminates the leak path while still working at small sizes where butt-welding is impractical. Butt-weld at small sizes is used when flow characteristics or full code-equivalence matters. Your piping engineer makes the call based on service, code, and assembly conditions.
Should I specify long radius or short radius elbows?
Long radius is the default for butt-weld elbows — the centre-to-end dimension is 1.5 times the nominal pipe size. Short radius elbows have a centre-to-end dimension equal to the NPS, used where space is constrained. Long radius gives smoother flow, lower pressure drop, and better erosion resistance, and is the standard spec unless layout forces short radius. If your bill of materials doesn’t specify, supply defaults to long radius. Threaded and socket-weld elbows don’t have a long/short radius option — they come as they are.
Do fittings need to match the pipe schedule exactly?
Yes, and this catches procurement teams more often than it should. Butt-weld fitting wall thickness is matched to the pipe schedule it’s welding into — Sch 40 fittings into Sch 40 pipe, Sch 80 into Sch 80. Mismatched schedules create welding problems and may not meet code. The complication is across alloys: if a project substitutes a higher-strength alloy at the same NPS but different wall thickness, the fitting schedule shifts too. Always confirm fitting schedule against pipe schedule before placing the order.
Can MTRs be supplied, and which fittings need CRN registration?
MTRs traceable to the heat number are available on request and routinely supplied for pressure-system and CRN-registered applications. They confirm chemical composition, mechanical properties, and conformance to ASTM A403 (butt-weld) or A182 (forged). On CRN: stainless fittings used in pressure systems in Alberta, BC, Saskatchewan, Ontario, and other provinces commonly require fitting-level CRN registration in addition to system registration. Stocked fittings carry registration where applicable. Confirm requirements for your jurisdiction and service at the time of quote.
Ready to Order or Need Help Sizing?
Our technical sales team can help you select the right size, material, and configuration for your application.